Medical Equipment Manufacturer Selection Guide for Global Buyers
How to Choose the Right Medical Equipment Manufacturer
Selecting the right medical equipment manufacturer is one of the most important decisions for hospitals, healthcare organizations, distributors, and international project contractors.
A medical equipment supplier does not only provide products. The manufacturer also affects equipment reliability, technical support, installation quality, maintenance efficiency, and long-term operating costs.
How can global buyers evaluate a medical equipment manufacturer before making a purchasing decision?
A professional evaluation should include:
manufacturing capability;
product expertise;
quality management;
technical support;
international experience;
after-sales service.
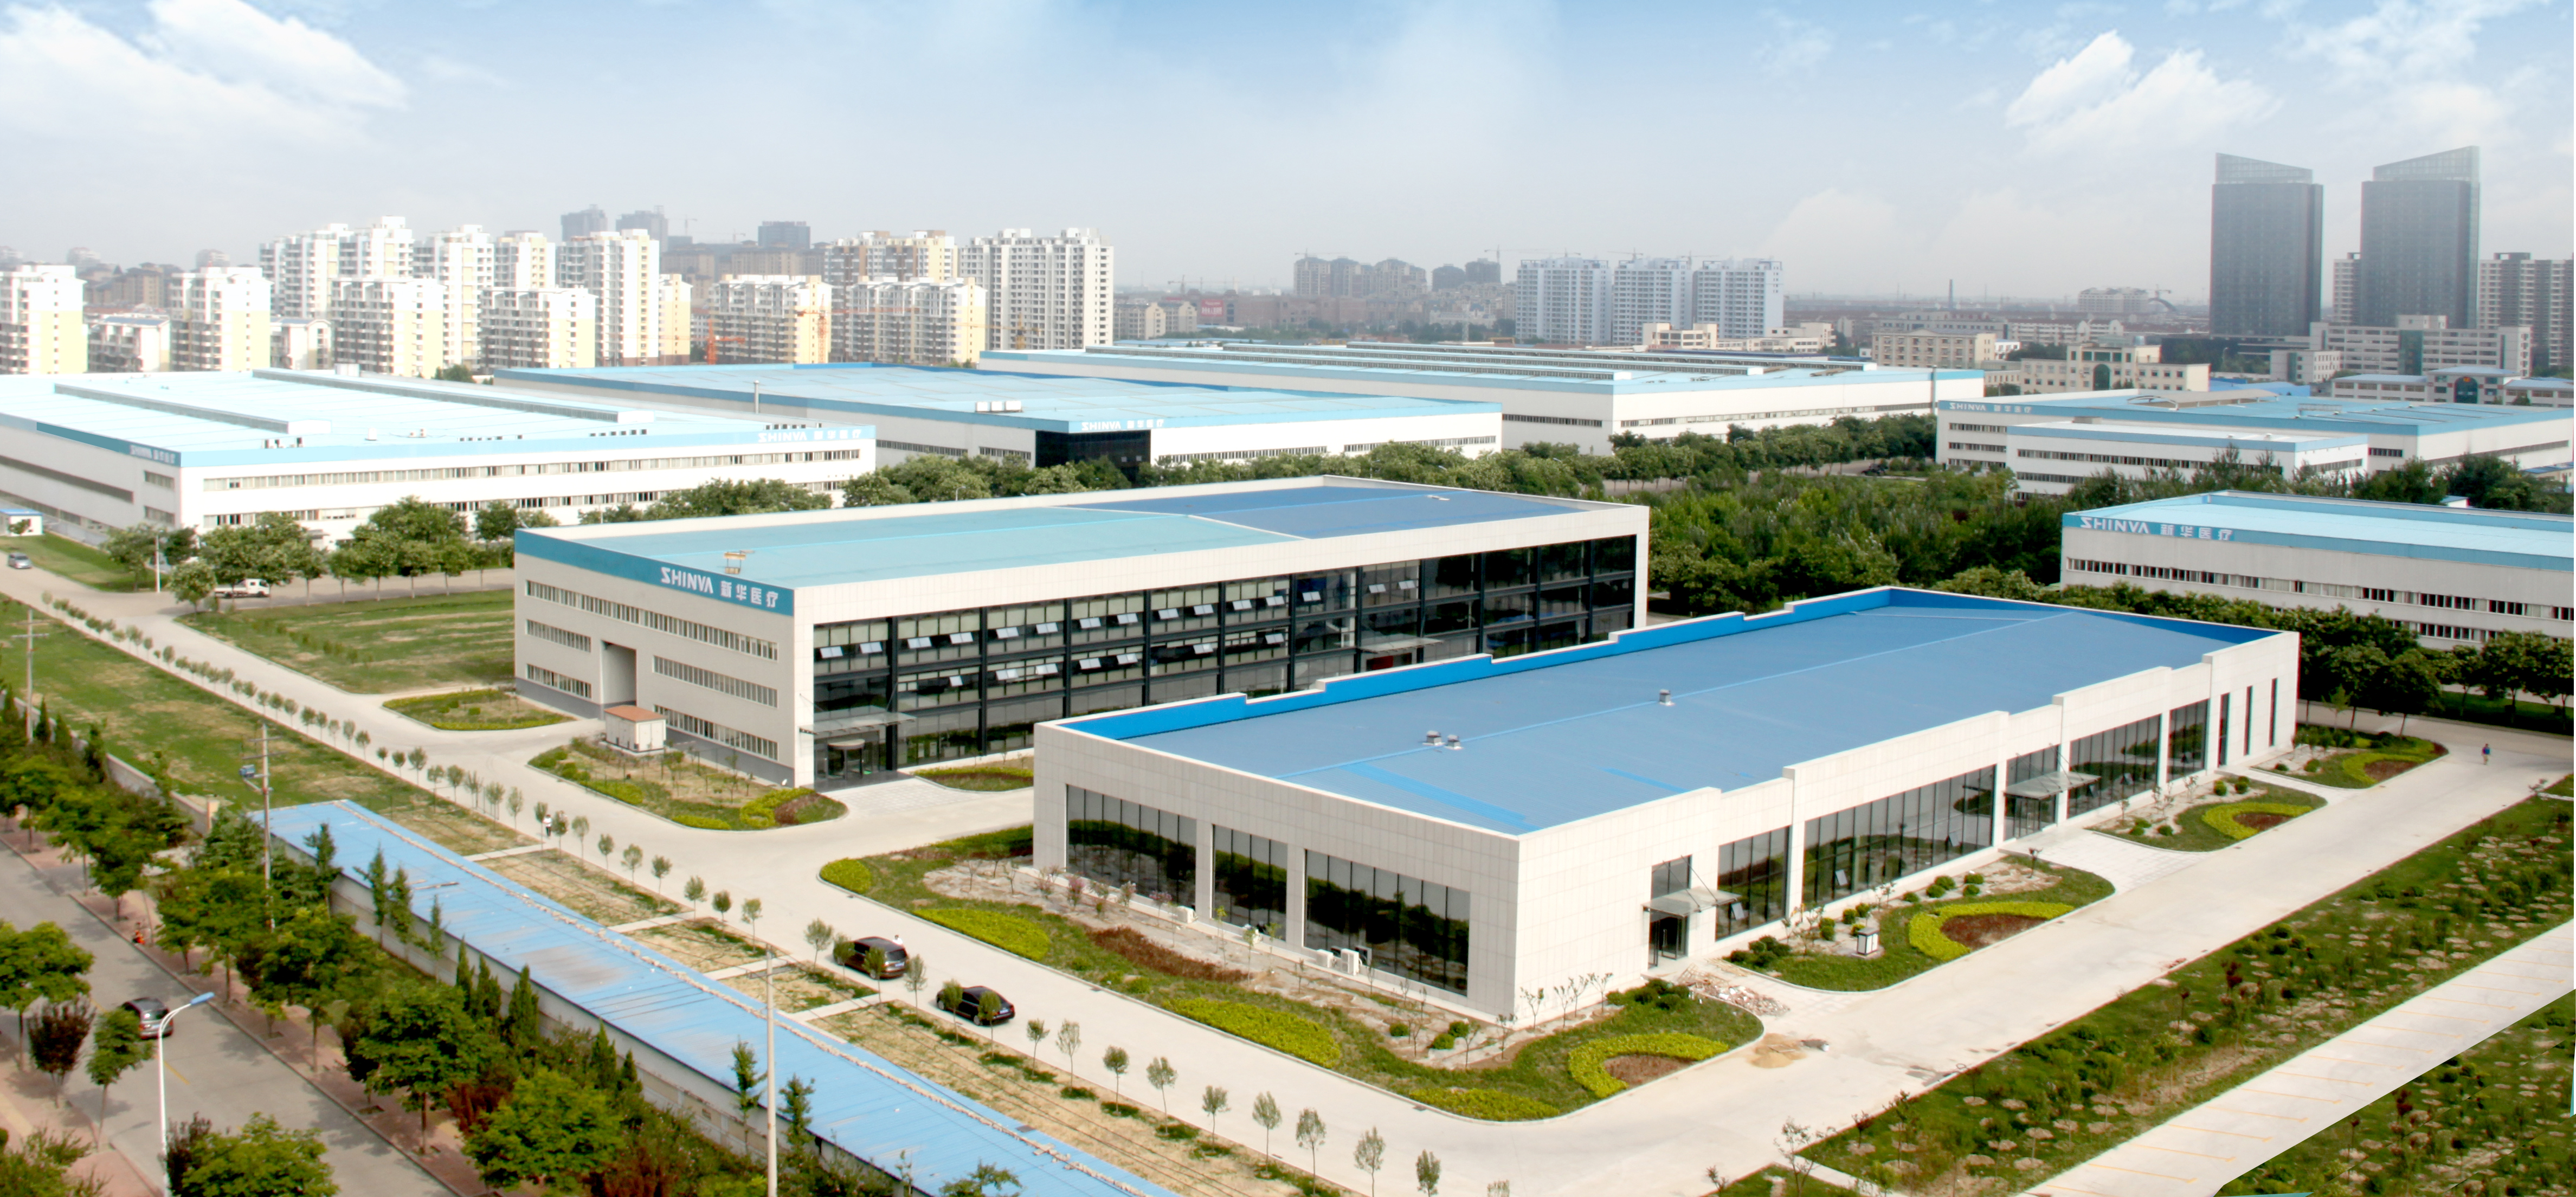
SHINVA has developed healthcare equipment solutions covering infection control, surgical instruments, radiotherapy systems, laboratory equipment, pharmaceutical equipment, and other medical technology fields.
Buyers can review the to understand different healthcare equipment categories before starting supplier evaluation.
This guide provides a practical checklist for selecting a reliable medical equipment manufacturer.
Why Choosing the Right Medical Equipment Manufacturer Matters
Healthcare equipment procurement is different from ordinary industrial purchasing.
Hospitals are not only buying machines.
They are investing in long-term healthcare infrastructure.
A suitable manufacturer should support the complete equipment lifecycle:
Product development
Manufacturing
Quality control
Installation
Training
Maintenance
Technical support
Choosing an unsuitable supplier may create problems such as:
delayed installation;
incomplete documentation;
limited technical support;
difficult spare parts management;
increased operating costs.
Therefore, manufacturer selection should happen before price comparison.
1. Evaluate Medical Equipment Manufacturing Capability
The first step is determining whether a company has real manufacturing capability.
Many companies can sell healthcare products.
However, fewer companies have complete medical equipment manufacturing experience.
Production Facilities and Manufacturing Processes
A qualified medical equipment manufacturer should have:
dedicated production facilities;
engineering teams;
quality inspection systems;
manufacturing procedures;
supply chain management;
testing processes.
Manufacturing capability directly affects product consistency.
For medical equipment, production control influences:
reliability;
service life;
maintenance requirements;
user experience.
Buyers should understand whether the supplier controls the production process or mainly acts as a reseller.
Engineering and Product Development Ability
A strong manufacturer should provide more than standard products.
Healthcare projects often require adjustments based on:
hospital layout;
workflow requirements;
department capacity;
local operating conditions.
Engineering capability allows manufacturers to support:
equipment configuration;
technical consultation;
project planning;
application optimization.
This is especially important for large hospitals and integrated healthcare projects.
2. Review Medical Equipment Product Expertise
A reliable manufacturer should understand the healthcare applications behind each product category.
Different medical fields require different technical knowledge.
Infection Control Equipment Manufacturing
Sterile processing requires complete workflow understanding.
Important equipment includes:
washer-disinfectors;
steam sterilizers;
endoscope cleaning systems;
sterile storage solutions.
SHINVA provides designed for sterile processing departments and healthcare facilities.
When evaluating an infection control manufacturer, buyers should review:
product range;
workflow knowledge;
installation capability;
maintenance support.
Surgical Instrument Manufacturing
Surgical instruments require precision manufacturing and specialty knowledge.
Important evaluation factors include:
material selection;
manufacturing accuracy;
instrument design;
specialty coverage;
sterilization compatibility.
SHINVA provides covering different surgical applications.
A capable manufacturer should understand not only how to produce instruments but also how they are used in clinical workflows.
Radiotherapy Equipment Manufacturing
Radiotherapy projects require more than equipment delivery.
They involve:
treatment workflow;
facility planning;
installation;
commissioning;
quality assurance;
maintenance.
For oncology projects, buyers should evaluate manufacturers with experience in .
The supplier should understand the complete project environment, not only the equipment itself.
Pharmaceutical and Laboratory Equipment Manufacturing
Pharmaceutical and laboratory projects often involve complex processes.
Manufacturers should understand:
production workflows;
contamination control;
sterilization requirements;
equipment integration;
facility conditions.
SHINVA provides for different pharmaceutical production applications.
3. Assess Quality Management Capability
Quality management is one of the most important factors when selecting a medical equipment manufacturer.
A reliable supplier should demonstrate how quality is controlled throughout the manufacturing process.
Quality Control During Production
Important quality processes may include:
incoming material inspection;
component verification;
assembly control;
functional testing;
final inspection;
documentation management.
Quality should be built into every manufacturing stage.
It should not depend only on final product inspection.
Technical Documentation and Traceability
Before cooperation, buyers should request:
technical specifications;
operation manuals;
installation documents;
maintenance guides;
product drawings;
spare parts information;
training materials.
Documentation supports:
installation;
operation;
maintenance;
regulatory preparation.
A professional manufacturer should provide clear and complete technical information.
4. Evaluate Technical Support Before Purchase
A medical equipment manufacturer should provide technical support before the order is placed.
Technical support helps buyers select the correct configuration.
Pre-Sales Engineering Support
Before final quotation, suppliers should understand:
application requirements;
workload;
installation environment;
workflow;
accessories;
future expansion.
A manufacturer that asks detailed technical questions usually has stronger project experience.
A simple product quotation may not address the actual healthcare requirement.
Customization and Project Solutions
Healthcare projects are rarely identical.
Different facilities may require different:
equipment configurations;
room layouts;
workflow designs;
capacity planning.
Manufacturers with engineering teams can provide better project solutions.
SHINVA provides integrated healthcare solutions across multiple medical fields through its .
5. Evaluate International Experience and Export Capability
For international buyers, manufacturing capability is only one part of supplier evaluation.
Global projects also require:
export experience;
documentation support;
communication ability;
installation coordination;
after-sales service.
Questions Global Buyers Should Ask
Before selecting a manufacturer, ask:
Which countries have you supplied?
Do you support overseas installation?
Can you provide technical training?
How are spare parts supplied?
Do you support local distributors?
How is after-sales service managed?
SHINVA states that its products have been exported to more than 110 countries and regions.
International experience can help manufacturers understand different project environments.
However, buyers should still confirm service availability for their specific market.
6. Manufacturer vs Distributor: Which Should Buyers Choose?
Many healthcare buyers work with either manufacturers or distributors.
The right choice depends on project complexity.
| Factor | Manufacturer | Distributor |
|---|---|---|
| Product development | Direct capability | Usually limited |
| Manufacturing control | Direct | Depends on supplier |
| Customization | Usually stronger | Depends on manufacturer |
| Technical communication | Direct engineering support | May involve multiple parties |
| Factory information | Direct access | Usually indirect |
| Large projects | Often preferred | Depends on capability |
For large hospitals and complex healthcare projects, direct manufacturer cooperation may provide advantages in:
technical communication;
customization;
project coordination;
lifecycle support.
7. Medical Equipment Manufacturer Evaluation Checklist
Before making the final decision, evaluate the supplier using these categories.
Manufacturing Capability
✓ Production facilities ✓ Engineering team ✓ Manufacturing experience ✓ Quality control process
Product Capability
✓ Suitable product categories ✓ Application knowledge ✓ Technical specifications ✓ Configuration flexibility
Quality Capability
✓ Documentation system ✓ Testing procedures ✓ Traceability ✓ Quality management
Service Capability
✓ Installation support ✓ Training ✓ Maintenance ✓ Spare parts
International Capability
✓ Export experience ✓ Global communication ✓ Distributor support ✓ Project experience
A structured checklist helps buyers compare suppliers objectively.
Common Mistakes When Choosing a Medical Equipment Manufacturer
Selecting Only Based on Price
A lower initial price may create higher long-term costs.
Consider:
maintenance;
downtime;
spare parts;
training;
technical support.
Ignoring Manufacturing Capability
A company selling equipment does not always have manufacturing expertise.
Verify production ability before cooperation.
Not Evaluating After-Sales Support
Medical equipment requires continuous support.
A reliable supplier should support the equipment lifecycle.
Choosing Equipment Without Considering Workflow
The best equipment is not always the one with the most features.
It is the one that fits the healthcare process.
Final Checklist Before Selecting a Medical Equipment Manufacturer
Before signing an agreement, confirm:
Manufacturing
Production capability reviewed
Quality processes understood
Engineering capability evaluated
Production capability reviewed
Quality processes understood
Engineering capability evaluated
Product
Equipment matches application
Technical requirements confirmed
Accessories included
Equipment matches application
Technical requirements confirmed
Accessories included
Project
Installation responsibilities defined
Training requirements confirmed
Acceptance process agreed
Installation responsibilities defined
Training requirements confirmed
Acceptance process agreed
Service
Maintenance plan available
Spare parts process confirmed
Technical support clarified
Maintenance plan available
Spare parts process confirmed
Technical support clarified
Conclusion: Choose a Medical Equipment Manufacturer as a Long-Term Partner
Selecting a medical equipment manufacturer requires more than comparing product specifications.
The right partner should provide:
reliable manufacturing capability;
technical expertise;
quality management;
product knowledge;
project support;
lifecycle service.
For hospitals, distributors, and healthcare projects, the manufacturer relationship continues long after delivery.
A professional manufacturer becomes a long-term technology partner.
Explore to understand healthcare equipment capabilities across different medical fields.
For specific project requirements, to discuss equipment selection, configuration, and support requirements.
Frequently Asked Questions
What should I look for in a medical equipment manufacturer?
Evaluate manufacturing capability, product expertise, quality management, technical support, international experience, and after-sales service.
What is the difference between a medical equipment manufacturer and supplier?
A manufacturer develops and produces equipment.
A supplier may include manufacturers, distributors, and service providers.
For complex projects, direct manufacturer support may provide stronger technical communication.
How can I verify a medical equipment manufacturer?
Review company background, production capability, technical documentation, quality processes, project experience, and service capability.
Why is manufacturing capability important for medical equipment?
Manufacturing capability affects product consistency, quality control, customization ability, and long-term support.
Should hospitals buy directly from manufacturers?
For large projects, direct cooperation may improve communication, customization, installation coordination, and lifecycle support.